

1. The place to insert the name of the working - For example, in working to make the workings more clearly defined, it is recommended to specify Lxxx - where L stands for the working length of the tool (the red line in the tool preparation) Rxx - where R means the working radius (x) - where it means the tool offset and Zxx - where it means the tool correction relative to the working length of the tool. E.g. L160 R49 (0) Z0
2. Name of the tool for that working
3. Working type - a place to choose the working type
4. Milling subtype - a place to choose the subtype of working
5. Working radius - The place to set the working radius. Note: All of the workings must have the same working radius
6. Azimuth angle - A place to set the angle of working
7. Sequence - the place to set the sequence of that working. Note: Better to set the sequence on profile logic to have more clear sequence of workings.
8. Machining hood - A place to set the hood position on machine
9. Machining hood 2 - A place to set the hood second position on machine
10. Develop 3d hole unidirectional - The working of a hole always starts from one point and goes in the same orientation
11. Do not empty breaking - External circular working (without working in central)
12. Calculate pocket path without using a final cleaning line - External circular working with working in central of pocket
13. Offset reference if piece overturned - Reference point when rotated element
14. Additional options - For example if working must be using for hardware the option utilizable for hardware must be ckecked
15. Colour - set the colour of working
16. Description - The place to set the description of that working
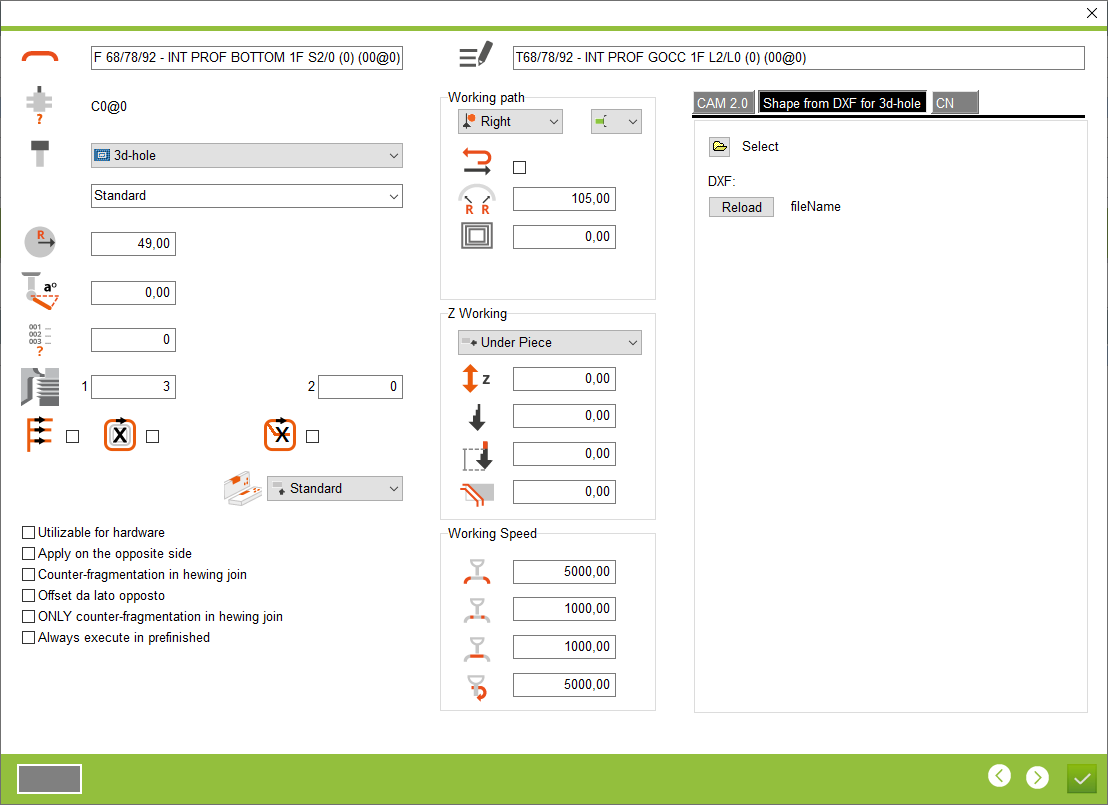


17. Working path - The place to choose the working path, if selected automatic, the tools going on correct way always when working on ends sides. Note: For tools like a drill or end mill must be choosen a path none then the path of the tool is calculated from its centre
18. Tool input/output type
19. Inversion - if selected the tool inverts the machining working
20. Input/output radius - Tool entry and exit radius, usually given as the maximum radius of the tool multiplied by 1.2
21. Z position of tool - Selection point for positioning the workings in relation to the under piece, over piece, half element, stop glass band thickness
22. Offset Z - Offset of tool relative to Z entered in tool definition
23. Z incremental - Note: Only for drill or end mill. Setting the incremental value for Z when drilling or end milling
24. Stretch to which the incremental working is applied - Value by which the tool input is skipped as an incremental (E.g. if there is no material for the first 10mm and we do not want the tool to go incrementally down to this value, so we can skip this value)
25. Incremental value for raw material - Place where you enter the value for how many millimetres you want to remove the raw material
26. In/Out speed - Tool input and output speed
27. Counter-fragmentation speed - Speed anti material break-out
28. Feed speed - Feed speed in the material
29. Rotation speed
30. CAM 2.0 - Place to set the working speed and category settings
31. CN - Tab with special CN codes for workings
32. Folder button - place to choose a DXF file for working
33. Reload button - button for reload a DXF file after changing
This is the place in the program where the user can configure the working, which is then applied to the individual profile logics.